Legal Update The District Court of The Hague has ruled in TwistR Energy's favour, confirming our position as the sole authorised commercial entity for Twister™ technology. Read more →
Proven Twister™ Technology · Since 2003

Gas separation
at the speed of sound

Twister™ supersonic technology dehydrates, dewpoints, and recovers NGLs from natural gas — with no chemicals, no moving parts, and no need for permanent operator presence. For the right project, it delivers transformational economics.

Twister™ is a static gas separation device that accelerates natural gas past Mach 2 through a converging-diverging nozzle, causing water vapour and heavy hydrocarbons to condense and separate — with no chemicals, no moving parts, and no emissions.

Live Reference — Offshore Malaysia

Shell B11 Platform · 600 MMSCFD Sour Gas

A Twister™ Supersonic Separator and Hydrate Separator system has been safely dehydrating highly sour natural gas on Shell's B11 production platform for more than 20 years — continuously, with near-zero maintenance.

600
MMSCFD
Throughput
20%
CO₂ Content
(highly sour)
3,500
ppm H₂S
Content
20+
Years of
Operation

"If you do what you always did,
you get what you always got."

The Conventional Alternative

Why conventional dehydration falls short

Traditional glycol-based and amine dehydration systems are complex, chemical-intensive, and demand permanent staffing offshore. They carry inherent H₂S exposure risks, significant CAPEX, and high ongoing maintenance requirements. Twister changes the equation entirely.

  • Continuous chemical supply chains (glycol, amines) and regeneration systems
  • H₂S exposure risks from chemical inventories on remote offshore platforms
  • Permanent operator presence required — high OPEX and HSE exposure
  • Large topside footprint and weight — expensive to engineer and build
5 Reasons to Consider Twister

A fundamentally different approach to gas conditioning

01

Extremely Stable Uptime

Extremely high and stable uptime, running for years without intervention. No pipeline integrity issues from chemical contamination.

>99%

Availability since 2003

02

Unmanned Operation

Twister requires virtually no maintenance and can be operated unattended. No moving parts means nothing to service or replace.

75%

Less operator intervention

03

No Regeneration Systems

Dehydration by supersonic expansion cooling requires no chemical regeneration systems, reducing both CAPEX and OPEX significantly.

50%

Typical CAPEX savings

04

Chemical-Free Process

No glycol or other chemicals needed. Less waste. Zero process emissions. A closed system — inherently safer for sour gas fields.

Zero

Process emissions

05

Smaller Plant Footprint

Twister reduces plant size by up to 70%. A single compact tube replaces entire equipment trains — saving weight, space, and structural cost.

70%

Reduction in plant size

How It Works

Supersonic physics.
Elegant engineering.

1

Acceleration to supersonic velocity

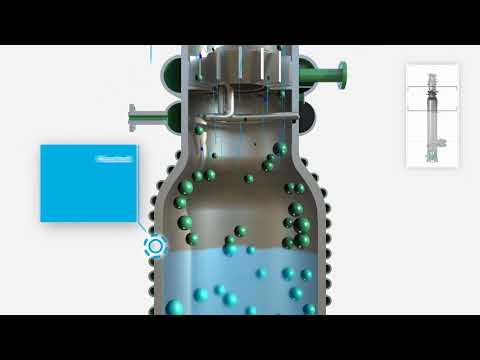
Wet gas enters a converging-diverging nozzle and accelerates past Mach 2, causing extreme temperature drop — well below the hydrocarbon and water dewpoints.

2

Condensation & swirl separation

Water and heavy hydrocarbons condense instantly. A powerful swirl forces liquid droplets to the outer wall of the tube, spinning them out of the gas stream.

3

Dry gas at pipeline specification

The dry gas exits through the inner tube. Liquids drain separately. The entire process takes place in a static device classified as standard piping — with no moving parts whatsoever.

The same CFD technology used in Formula 1 aerodynamics is applied to model gas behaviour at the molecular level, enabling precise engineering for any gas composition, pressure, and temperature.

WET GAS IN DRY GAS OUT LIQUIDS MACH > 2 SUPERSONIC ZONE
Watch It in Action

See the technology explained

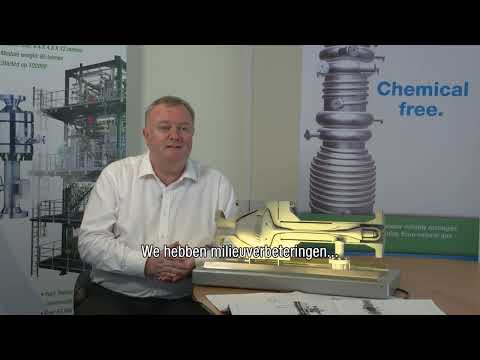
Two short videos that show how Twister™ supersonic separation works in practice — including a segment from Dutch national television.

Twister supersonic separator — technology explanation
Technology Overview
How Twister™ supersonic separation works
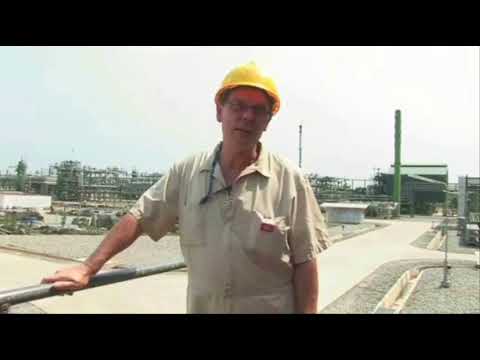
Twister — Dutch television feature
As seen on Dutch national television
Twister technology — broadcast feature
Applications

The same answer for every gas processing challenge

Twister™ technology addresses dehydration and dewpointing challenges in a flexible, cost-effective and sustainable way — whether greenfield or brownfield, onshore or offshore, sweet or sour gas. One technology, multiple proven applications.

Offshore (Sour) Gas Dehydration

Proven with up to 20% CO₂ and 3,500 ppm H₂S. Safer and simpler than glycol platforms — no chemical inventories, no emissions.

Offshore (Sweet) Gas Dehydration

Annual savings of up to US$50 million on a 300 MMSCFD offshore dehydration unit. Reduced platform weight by up to 50%.

Onshore Gas Dehydration & Dewpointing

A single unit processes 30 MMSCFD, achieving water and hydrocarbon dewpoints simultaneously. Flexible in remote locations.

NGL Recovery

Near-isentropic expansion achieves deeper cooling than turbo-expanders and JT systems, recovering significantly more C3+ NGLs.

Condensate Stripping & Gas Reinjection

Offshore light oil/condensate stripping with NGL recovery rates of up to 25,000 BPD and integrated gas reinjection.

FLNG & Membrane Pretreatment

Simultaneously dehydrating and removing hydrocarbons for FLNG bulk pretreatment, significantly reducing topside complexity.

Live Reference Case

Shell B11 Platform,
Offshore Malaysia

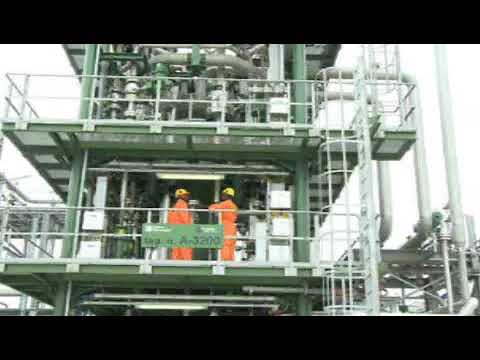
For more than 20 years, a Twister™ designed offshore dehydration system combining the Twister Supersonic Separator and Hydrate Separator has been safely dehydrating 600 MMSCFD of highly sour natural gas on Shell's B11 production platform in Malaysia.

The gas contains up to 20% CO₂ and 3,500 ppm H₂S — among the most challenging sour gas environments in the world. Twister was selected as a key element of Shell's sour gas risk mitigation strategy, providing an inherently safer closed system over traditional glycol-based dehydration.

The installation has operated continuously with near-zero maintenance and no permanent operator presence required on the processing system, delivering the promised economics from day one.

600
MMSCFD throughput — one of the world's largest offshore gas dehydration installations
20+
Years of continuous operation with no major interventions
20%
CO₂ content — extreme sour gas environment, 3,500 ppm H₂S
40%
CAPEX savings versus conventional glycol-based platform design
In their own words

Hear from engineers who chose Twister

Engineers evaluating Twister technology speak directly — about performance, integration, and what it means for field operations.

Engineer testimonial
Team

The people behind TwistR Energy

Our team combines deep expertise in gas processing, thermodynamics, engineering and international energy markets.

Pieter Kapteijn

Pieter Kapteijn

Co-founder · CEO & Technical

Co-founder and CEO of TwistR Energy, leading technical design and commercial delivery of Twister™ supersonic separation systems. After 28 years at Shell E&P — spanning production technology, R&D leadership, Smart Wells implementation and Smart Fields programme direction — Pieter served as Director of Corporate Technology and Innovation at Maersk Oil, then as CTO at Sierra Oil and Gas, Mexico's first independent oil company. He co-founded Marine Performance Systems, whose air lubrication technology was acquired by Alfa Laval (now marketed as OceanGlide). He brings a 45-year track record of engineering innovation and technology commercialisation to TwistR's mission.

LinkedIn profile
Gabriël de Scheemaker

Gabriël de Scheemaker

Co-founder · CFO & Commercial

Co-founder and CFO of TwistR Energy, responsible for strategy, corporate development, and commercial structuring of new projects. A former Shell executive with 35 years of energy experience, he has co-founded and financed deep-tech energy ventures in hydrogen storage, advanced batteries, algae biofuels, and CCUS. He brings the financial rigour of a Shell career — including CFO of Shell Hydrogen and founding member of Shell Capital — to TwistR's mission of deploying proven supersonic separation technology at commercial scale. MSc Electrical Engineering (TU Delft) · MBA International Finance (NYU Stern).

LinkedIn profile
Varun Venkateswaran

Varun Venkateswaran

Technical Manager

Computational Fluid Dynamics specialist (Ansys Fluent, TU Delft) with sharp expertise in supersonic flow simulation and a talent for quickly matching Twister technology to specific customer requirements.

LinkedIn profile
News

Latest from TwistR Energy

FAQ

Common questions about Twister™ technology

Technical and commercial questions answered directly — from how supersonic separation works to CAPEX savings, sour gas capability, NGL recovery, and CO₂ capture.

View all questions
What is Twister™ supersonic gas separation?
A static device that accelerates gas past Mach 2, causing water and heavy hydrocarbons to condense and separate — with no chemicals or moving parts.
Does Twister™ work for sour gas?
Yes. Proven 20+ years on Shell B11 with up to 20% CO₂ and 3,500 ppm H₂S — one of the most challenging sour gas environments in the world.
Can Twister™ be used for CO₂ capture?
A new CO₂ separation product line is under development for hard-to-abate industries, using consortium-funded joint development to reach full commercial deployment.
Contact

Is Twister right for your project?

Twister technology delivers transformational results for the right applications — but it is not the right solution for every project. We are happy to evaluate your specific conditions and be direct about whether Twister adds value for you.

Get in touch with a brief description of your application — gas volumes, composition, location and processing objectives — and we will respond with a frank technical assessment.

Headquarters
The Netherlands
Active Regions
Africa · Asia Pacific · Middle East · South America

Send us a message

For project enquiries, technical questions or investor discussions, reach us directly by email. We aim to respond within one business day.

TwistR Energy on LinkedIn